If you’re running a food processing plant, you already know that even a tiny hygiene misstep can shut down your entire operation—remember that time a minor contamination scare led to a full plant audit and days of lost production? Yeah, we’ve heard the horror stories firsthand, and as a hot oil boiler supplier, we see how easy it is to overlook the unique hygiene rules for these systems. Unlike steam boilers that use water, hot oil boilers circulate heat-transfer oil to cook, dry, or pasteurize everything from snack chips to fruit puree, so any gunk, bacteria, or degraded oil in the system can end up in your final product. No pressure, but this isn’t just “boiler maintenance”—it’s the make-or-break between hitting your hygiene targets and getting a full recall. Let’s break down the non-negotiable hygienic requirements we train every client on, straight from the teams that help food plants avoid shutdowns. Hot Oil Boiler
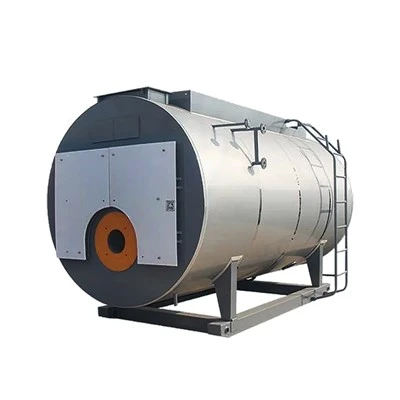
First off, the oil itself—this is the backbone of your system, and it’s way more than just fluid to move heat around. Food-grade hot oil isn’t a random oil you pick up at a grocery store shelf; it has to meet specific standards (more on that later) and you’ve got to keep it from breaking down. When oil overheats, it starts to oxidize, forming sludge, acids, and varnish that cling to boiler walls, pipes, and even strainers. That gunk isn’t just bad for your boiler efficiency—it’s a petri dish for bacteria, and if it gets into your product lines, it’s a huge red flag. We always tell clients to track two things here: oil temperature and total acid number (TAN). TAN measures how acidic the oil is, and for food-grade systems, you’ve got to keep that TAN below 0.5 mg KOH/g, no exceptions. If it climbs higher, the oil’s done—replacing it isn’t cheap, but it’s way cheaper than recalling a batch of cookies or sauces. Also, never mix different types of hot oil. Some plants try to stretch oil life by adding in leftover old oil from a different brand, but even if they’re both food-grade, their additives can react, forming that sludgy gunk we talked about. We’ve had a client learn this the hard way: they mixed two oils and ended up with a clog so bad they had to drain and replace the whole system, costing them $120k in downtime. Lesson learned, right?
Next up, pre-use validation—this is the step most new plant owners sleep on, and it’s critical to avoiding contamination from day one. When you install a new hot oil boiler, or even after a big repair, you can’t just fire it up and start running your snack line. You’ve got to do a full passivation of the system first. Passivation is basically treating the metal surfaces (boiler tubes, pipes, heat exchangers) to create a clean, non-reactive layer so oil doesn’t stick and bacteria don’t have places to hide. If you skip this, the leftover cutting oils, welding slag, or metal dust from installation will mix with your hot oil and end up in your product. We walk clients through this every time: flush the system with a food-safe solvent (not just water, because hot oil systems are almost always closed, so water can cause rust), then run the oil through multiple high-efficiency filters during start-up, and test for particulate matter before even thinking about pumping it to your process lines. One craft bakery we work with tried cutting corners on this, and their first batch of croissants had a metallic off-flavor that led them to throw out 500 dozen pastries. That lost revenue would’ve paid for a full passivation three times over.
Then there’s regular system cleaning and inspection, which isn’t a “set it and forget it” task. Hot oil systems build up that varnish and sludge over time, especially on the heat transfer surfaces, and those spots are impossible to reach with just a simple flush. We recommend two types of cleaning: on-line cleaning for minor buildup and annual (or semi-annual) full system cleaning with food-grade chemical cleaners, depending on your plant’s throughput. On-line cleaning uses a circulation of a low-foaming, food-safe detergent that breaks down gunk without having to shut the whole plant down for a week—perfect for plants that run 24/7. But even that can’t get all the buildup out of the boiler tubes, so you’ve got to pull the boiler head once a year to inspect for scale or sludge. If you let sludge build up too much, it insulates the tubes, making the boiler work harder, and also creates dead zones where oil stagnates. Stagnant oil is a huge hygiene risk—bacteria thrive there, and it breaks down much faster than moving oil. We’ve also noticed that a lot of plants forget to clean the expansion tank and the overflow lines. The expansion tank is where extra hot oil goes when it heats up, and moisture can get in there over time, leading to oil degradation and rust. If that rust flakes off, it can clog filters or get into your process lines. It’s a tiny part of the system, but it’s one of the most common hygiene blind spots.
Moisture control is another big one—hot oil and water don’t mix, not when you’re dealing with food safety. Hot oil has to stay completely dry, because even a tiny bit of water (like 100 parts per million) can cause two problems: first, it will make the oil boil at high temperatures, leading to foaming, which can push oil into process lines. Second, water accelerates oil oxidation, making that TAN spike way faster than normal. How do you keep moisture out? Most food-grade hot oil boilers have a dry gas seal on the system—usually nitrogen or compressed air—to prevent humid air from getting in when you add oil or open the system for maintenance. We always remind clients to check that seal pressure daily; if it drops, moisture can sneak in, and you might not even notice until your TAN test comes back high. Also, never add water to a hot oil boiler, obviously, but even spills from washing nearby equipment can seep into the system’s lines if you’re not careful. One produce drying plant had a worker spill a bucket of water near the boiler’s pump, and over two days, that small amount of water got pulled into the system. By the time they noticed, they had to replace 3,000 gallons of hot oil and shut down for 18 hours to fix the rust that formed in the tubes. Avoidable, right?
Filtration is non-negotiable too, and not just any filter will do. You need high-efficiency particulate air (HEPA)-grade filters for the hot oil system, with a rating of at least 10 microns—some plants even go down to 1 micron for critical processes like pasteurizing dairy or mixing batters. The filters catch sludge, metal particles, and other contaminants before they get to your heat exchangers or process lines. We recommend changing them every 200 hours of operation, but if your plant processes high-fiber foods (like cereals or grain-based snacks) that can shed particulate matter, you might need to change them every 120 hours. Also, don’t forget to dispose of used filters properly—throw them in sealed, labeled containers so contaminants don’t spread, and make sure the waste hauler you use is certified to handle industrial food-related waste. It’s not just about keeping your plant clean; it’s about not contaminating other facilities down the line.
Another often overlooked rule: training your team. Even if you have the best boiler on the market, if your operators are cutting corners on tests or maintenance, you’re still at risk. We don’t just sell boilers—we run free training sessions for all our food plant clients on hygiene protocols, because we’ve seen too many good systems go bad because of human error. For example, one client’s operator was supposed to test TAN every week, but he forgot for three weeks because he was busy with a big product launch. By the time he noticed, the oil had broken down, and they had to replace the whole system, costing them more than $150k in downtime and oil. So training should be ongoing—monthly refreshers, quick check-ins, making sure every operator knows exactly what to test, how often, and what numbers are red flags. We also recommend assigning a dedicated hygiene lead for the boiler system, someone who’s responsible for logging all test results, scheduling maintenance, and auditing the system monthly. It’s a small role, but it takes the guesswork out of who’s in charge.
Wait, can we talk about regulatory stuff too? Because if you’re in the food industry, you’re dealing with FDA, EFSA, or other local food safety rules, and your hot oil boiler hygiene has to line up with those. The FDA’s Food Safety Modernization Act (FSMA) requires that you have a preventive control plan for all equipment that comes into contact with food, and hot oil systems are definitely in that bucket. EFSA has specific limits for food-grade heat-transfer oils, like the ones that ban certain additives that could be toxic if they get into food. So whatever boiler or oil you use has to be certified to meet those standards—no exceptions. We only work with suppliers that have their oils and boilers third-party certified for food safety, because we don’t want our clients getting hit with a fine or a shutdown because we cut corners. If you’re not sure what regulations apply to your plant, we can help you map that out too, no sales pitch required—just real guidance.

Let’s wrap this up with a quick reality check: hygiene for hot oil boilers isn’t something you do once and forget. It’s a daily routine, weekly tests, annual deep cleans, and ongoing training. Skip even one part of it, and you’re risking everything you’ve worked for—your product quality, your reputation, your bottom line. If you’re in the market for a new hot oil boiler, or you’re worried your current system isn’t meeting hygiene standards, we’re here to help. We don’t just sell equipment; we partner with food plants to make sure their systems are safe, efficient, and compliant, so you can focus on making great food, not stressing about boiler contamination. Hit us up to chat through your specific needs, whether you’re a small craft bakery or a large-scale snack manufacturer. We’ll help you build a hygiene plan that fits your plant, no jargon, no fine print, just real advice from people who know the food industry.
LNG Refueling Station References:
- Food and Drug Administration (FDA). (2023). Food Safety Modernization Act (FSMA) Preventive Controls for Human Food: Equipment Sanitation Requirements.
- European Food Safety Authority (EFSA). (2022). Scientific Opinion on the Safety of Heat-Transfer Oils for Use in Food Processing.
- American Society of Mechanical Engineers (ASME). (2021). Standard for Thermal Fluid Systems in Food and Beverage Processing Facilities.
- National Sanitation Foundation (NSF). (2020). Standard 61: Drinking Water System Components – Health Effects, and Standard 21: Food Equipment Materials for Heat Transfer Applications.
- International Food Protection Training Institute (IFPTI). (2022). Hot Oil Boiler Hygiene Protocols for Small and Medium Food Processing Plants.
Xinxiang Huayuan Container Equipment Co., Ltd.
With abundant experience, we are one of the most reliable hot oil boiler manufacturers and suppliers in China. We warmly welcome you to buy durable hot oil boiler made in China here from our factory. If you have any enquiry about cooperation, please feel free to email us.
Address: No.2, South Road, Industrial Cluster Zone, Genghuang Township, Fengquan District, Xinxiang City, Henan Province
E-mail: cncd527@gmail.com
WebSite: https://www.huayuanequipment.com/
