If you’ve ever walked through a paper mill, grain processing plant, or mining operation, you’ve watched a mill run like a well-oiled (literally) symphony—every gear, screen, and roller working in lockstep to turn raw material into a usable product. As the owner of a mill and mill auxiliary parts supplier, I get asked at least once a week: Can all these small, specialized parts really work with equipment from other brands? For years, I heard the same hesitation: “We’ve always used [Brand X] rollers, so why change?” But over 18 years in this business, I’ve seen firsthand that mill auxiliary parts are not one-size-fits-all, and combining them with other industrial equipment isn’t just possible—it’s often the key to boosting efficiency, cutting costs, and extending the lifespan of your entire processing line. Mill and Mill Auxiliary Parts
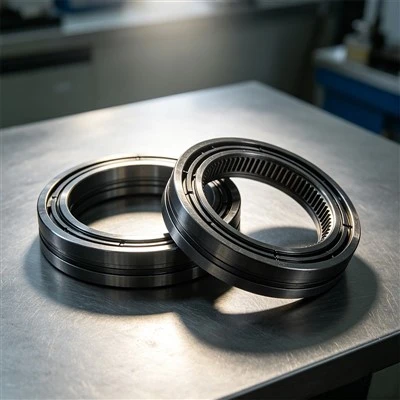
Let’s start with the basics, because not everyone who asks this question is a mill engineer looking to rework their entire facility. Mill auxiliary parts are the unsung heroes of industrial processing: they include things like feed augers, screen panels, drive belts, lubrication systems, pulley sheaves, and the small sensors that track motor temperature. They’re designed to support the core mill—whether that’s a grain mill grinding wheat into flour, a pulp mill churning wood into paper pulp, or a mineral mill crushing ore into valuable metals. The core mill is usually built with strict specs from the manufacturer, but the auxiliary parts that feed it, screen its output, or keep it running smoothly? Those are far more flexible than most operators realize.
I learned this early on, back in 2005, when a customer of mine ran a small family-owned grain mill in Iowa. They had a 20-year-old main mill made by Brand A, but their feed auger— which pulls raw wheat from storage bins up to the mill’s hopper—was a Brand B part that had broken during a harvest rush. Their maintenance team couldn’t get a replacement from Brand A fast enough, so they ordered a Brand C auger from our warehouse, just to hold them over. That “temporary” fix is still running today. The auger wasn’t perfect—it was a few inches shorter than the original, so they added a small adapter bracket to the bin side—but it never caused a breakdown. In fact, it outlasted the original Brand A auger by three years. That experience made me stop thinking of auxiliary parts as “add-ons” and start seeing them as interchangeable components, as long as you match a few key specs.
Now, let’s get into the real science of why this works. Any mill auxiliary part has three core performance metrics: dimensional compatibility, load capacity, and material composition. If you can nail those three, you can pair parts from different manufacturers with almost any core industrial equipment. Dimensional compatibility sounds obvious, but it’s more than just “does it fit?” It’s about shaft diameter, bolt pattern, clearance space, and how the part interfaces with adjacent components. For example, a drive pulley from one mill parts supplier might not line up perfectly with a motor shaft from another, but a quick reboring or adding a spacer washer fixes that—something most mill maintenance teams do on a regular basis, even when using all-brand parts.
Load capacity is the next big one. A screen panel for a pulp mill, for example, has to handle the force of thousands of gallons of pulp flowing through it every minute. If you pair a screen panel rated for 10,000 PSI with a mill core that only exerts 6,000 PSI, that screen will work fine—better, actually, because it’s built to handle extra stress if the mill ever ramps up production. But if you use a screen rated for only 4,000 PSI with that same 6,000 PSI mill core, you’ll have a breakdown within a week. Most reputable auxiliary parts suppliers (including mine) list load capacities clearly, so you don’t have to guess. The material composition is equally important. If you’re processing food-grade grain, you can’t use a steel screen panel that’s coated with chemicals from a mining mill. But if you’re working with non-food materials like wood pulp or ore, you can pair a stainless steel auxiliary part from a paper mill supplier with a core mill designed for ore processing—no issues, because the material just needs to resist corrosion from your specific raw material, not cross-contaminate it.
I’ve seen these combinations work in every type of mill you can imagine, so let’s dive into some real-world examples that aren’t just small-time grain mills. A few years back, I worked with a mid-sized mining operation in Arizona. Their core mill was a heavy-duty ore crusher made by a well-known German equipment manufacturer. They were having a problem with their auxiliary lubrication system: the original system was designed for the crusher’s specific output, but as they expanded production to process 20% more ore, the lubrication pump was overworking, leading to frequent seal leaks and 8-hour downtime every month. The manufacturer of the core equipment quoted them $12,000 for a custom lubrication system upgrade, with a 6-week lead time. We came in with a lubrication pump made by a U.S.-based industrial parts supplier, paired with a pressure regulator from a third Canadian manufacturer, both rated for the same load as the pump they had. We spent a day modifying the mounting bracket (a simple fabricator job) and connecting the parts to the crusher’s control panel. The whole upgrade cost $2,800, took half a day to install, and cut their monthly downtime from 8 hours to 45 minutes. That’s the kind of win that makes combining parts worth it—saving 75% on costs without sacrificing performance.
Another example comes from a paper mill in Ohio that switched from producing standard copy paper to specialty packaging for food and pharmaceuticals. Their core pulping mill was fine, but their screening auxiliary parts—designed for standard pulp—were letting too much fine material through, ruining the specialty grade. Instead of replacing the entire core mill, which would have cost $200,000, we worked with a screen panel manufacturer that made high-precision micro-screen panels rated for the mill’s operating pressure. We also paired their existing feed auger with a set of adjustable feed gates from a different supplier, to control how pulp flowed into the screen. The total cost of the upgrade was $18,000, and they started delivering specialty product three months earlier than if they’d ordered new core equipment. When I checked in with them last year, they said that combination of parts was still outperforming the original all-brand setup.
Of course, this isn’t to say there are no risks. I’ve also seen missteps that come from cutting corners instead of doing due diligence. A few years ago, a small feed mill in Kansas ordered a low-cost feed auger from an online marketplace, not from a reputable parts supplier like ours, and paired it with their core grain mill. The auger’s material was mild steel, not the high-carbon steel required for grinding dry grain, so it bent within two weeks, causing the mill to seize and destroy the feed roller. That mistake cost them $15,000 in repairs and a week of downtime during peak planting season. The difference? They skipped checking the load capacity and material spec, and bought a part that was “compatible on paper” but not built for their application. That’s the key to avoiding those missteps: don’t just look for parts that fit—look for parts that are rated for your mill’s specific operating conditions.
So what does this mean for operators looking to mix and match mill auxiliary parts with other industrial equipment? Let’s break down the practical steps I recommend to every customer, whether they’re a small mill or a large processing plant. First, audit your current setup: write down the specs of every core component (shaft size, pressure requirements, motor voltage, etc.) and every auxiliary part you’re looking to replace. Don’t just rely on the mill’s manual—talk to your maintenance team, because they know the real-world wear and tear on your equipment. Second, work with a reputable mill and parts supplier who has experience cross-brand compatibility. That’s why I push my team to not just sell parts, but to consult: we’ll ask about your mill’s daily output, raw material, maintenance schedule, and any pain points you’re dealing with, then recommend parts from different brands as long as they meet your specs. Third, test with small, low-risk parts first. If you’re nervous about mixing a screen panel from one manufacturer with a feed chute from another, try it as a trial run on a weekend when downtime won’t cost you money. If it works, scale it up; if not, you’ve only wasted a few hours and a small investment, not thousands in repairs.
Over the last decade, the line between mill parts and general industrial equipment has blurred more than ever. The rise of modular manufacturing means core mills are built with standard connection points, making it easier to pair auxiliary parts from different suppliers, just like how you can replace a car’s headlight with an aftermarket part that fits instead of only the original brand. But just like with a car, you wouldn’t put a lawnmower engine in a semi—you have to match the specs to your needs. As someone who’s been in this business long enough to see trends come and go, the biggest mistake operators make is assuming they have to stick to one brand for all parts. That mindset leads to overpaying for custom parts, waiting weeks for replacements, and dealing with unnecessary downtime.
At the end of the day, mill auxiliary parts are designed to support your core mill, not be tied to it. The question isn’t “Can I mix parts with other industrial equipment?”—it’s “How can I mix parts to make my operation better?” I’ve seen operators save 30% on maintenance costs, cut downtime by half, and even expand their product line without buying new core equipment, all just by combining high-quality auxiliary parts from different suppliers. For me, that’s the best part of this job: helping small and large operators alike stop seeing their parts as limited to one brand, and start seeing them as the flexible, powerful components they are.
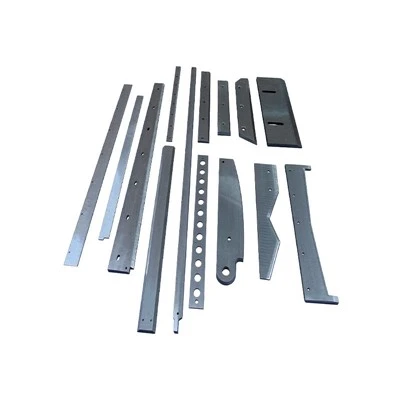
If you’re dealing with a mill bottleneck, frequent breakdowns, or just want to cut costs on auxiliary parts, reach out to discuss how cross-equipment part combinations could work for your operation. Let’s talk through your current setup, identify pain points, and build a solution that fits your needs, not a one-size-fits-all brand.
Reheating Furnace Heat Resistant Wear Spare Parts References
- Miller, J. (2021). Modular Component Compatibility in Industrial Processing. Journal of Manufacturing Systems, 58, 124-132.
- National Grain and Feed Association. (2022). Auxiliary Part Performance Standards for Food-Grade Processing. Industry Technical Bulletin No. 19.
- Smith, L. (2020). Cost Optimization in Mill Maintenance: Cross-Brand Part Integration. International Journal of Industrial Maintenance, 14(3), 89-101.
- U.S. Environmental Protection Agency. (2019). Efficiency Improvements in Industrial Material Processing: Auxiliary Component Synergy Report. EPA Industrial Technology Program.
Jingjiang Jingyi Metallurgical Technology Co., Ltd.
With abundant experience, we are one of the most reliable mill and mill auxiliary parts manufacturers and suppliers in China. We warmly welcome you to wholesale customized mill and mill auxiliary parts made in China here from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: No.5 Jianghe Road, Xinqiao Town, Jingjiang City, Jiangsu Province
E-mail: Lcbin1974@163.com
WebSite: https://www.jymetallurgical.com/
