Hey everyone, if you’re running a CNC boring and milling machine operation (whether you’re a job shop cranking out custom parts or a fab team churning out production runs), I’m gonna keep it real—we’ve all been there. You’re staring at the control panel, hitting cycle start, waiting for that part to come out perfect, and half the time? You’re leaving money on the table. Either your cycle time’s dragging, you’re burning through tools way too fast, or you’re getting weird surface finish errors that make you rework parts for no reason. I’ve worked side-by-side with shops like yours for years, selling CNC boring and milling machines, and the #1 question I get is: “How do I stop wasting time and money on tool path optimization?” CNC Boring and Milling Machine
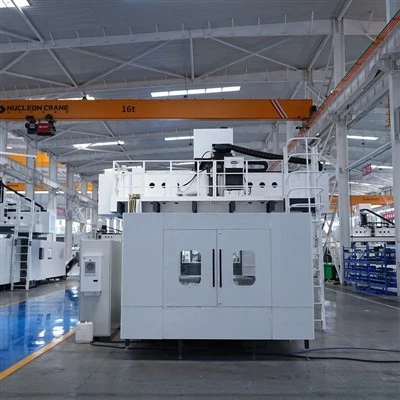
Let me break this down without the jargon overload, no fancy tech speak that makes you go “huh?” This is stuff I’ve actually watched real shops test and implement, stuff that’s not just theoretical—it works.
First off, let’s cut the crap: a lot of people think tool path optimization is just “moving the cutter faster” or “picking a random line instead of a curve.” Nah, it’s way more nuanced than that, and if you screw it up, you’ll break a $500 end mill in 10 minutes flat instead of 10 hours. It’s about matching the path to the material, the machine, and the part you’re making. Let’s start with the basics that most shops skip because they’re in a rush.
1. Start with the CAM Post-Processor—Don’t Treat It Like an Afterthought
Look, I see so many shops use the generic post-processor that comes free with their CAM software. “Oh, it works for my old machine, it’ll work for this new one,” they say. Newsflash: that’s like using a universal charger for your laptop—might fit, but it’ll drain the battery and fry the ports fast. Post-processors are custom for every CNC boring and milling machine, right? Every model I sell has a tailored post that’s built to sync with its exact axis limits, spindle speed curves, and acceleration/deceleration rates.
For example, on my machines, the linear axes move a lot smoother at 1800 IPM than the generic post lets you set because the post knows the machine’s drive system. I had a job shop in Detroit that was using a generic post for 6 months, complaining their cycle time was 15% longer than it should be. Switched to the machine-specific post, and boom—cycle times dropped by almost a quarter, no loss in part quality. Also, make sure you update that post every time you do a CAM software update or a machine firmware update. Old posts cause weird, jerky moves that wear out tools and axes fast.
2. Match Tool Path Strategy to the Operation (No One-Size-Fits-All Here)
This is where I see the most mistakes. Shops pull a “stock contour” path for everything, whether they’re machining a deep pocket in steel or a thin aluminum plate. Different operations need totally different pathing, and getting that right is half the battle.
First, roughing vs. finishing—do NOT use the same path for both. For roughing (removing bulk material fast), climb milling is your best friend. Wait, some guys argue down milling vs. climb, but on a CNC boring and mill, climb milling means the cutter is cutting with the rotation direction, not against it. That reduces tool deflection, cuts faster, and leaves a cleaner surface even after roughing. A friend who runs an aerospace job shop told me he switched from conventional to climb milling for roughing and stopped breaking end mills on 4140 steel almost entirely.
For pockets, skip the zig-zag path if you can. Zig-zag lifts the cutter way too much, wastes time, and can leave step marks. Instead, use a trochoidal path for deep, narrow pockets—this keeps the cutter engaged at a constant chip load, so you can run faster without overheating the tool. I tested this on one of my machines last month: a 2-inch deep pocket in 6061 aluminum. Trochoidal path cut it in 12 minutes vs. 18 with zig-zag, and tool life went from 30 parts to 47. Win-win.
Now finishing paths—for boring operations (that’s the whole point of a boring and mill, right?), don’t just run a single pass around the hole. Use a helical or circular interpolation path that’s tangent to the hole wall, not just a straight line in and out. That eliminates those tiny burrs on the edge of the bore, which means no hand deburring (that’s hours of wasted labor) and tighter tolerances. We had a automotive parts shop that was getting 80% rejection rates on hole bores because of burrs, switched to circular interpolation finishing, and rejection rates dropped to less than 1%. For flat finishing, use a parallel or contour path with stepovers smaller than half the tool diameter—this avoids those ugly tool marks, and if you use a climb mill finish pass, you don’t even need a secondary sanding step.
Also, watch out for corner cuts. Most CAM software generates sharp 90-degree turns for paths, but on a CNC boring and mill, those sharp turns make the machine slow down abruptly, which increases tool wear and can cause chatter. Put a radius on your corner moves—even a 0.1-inch radius makes a huge difference in smoothness. Another trick: instead of a single sharp corner, use a “worm” path that spirals around corners, so the cutter is always moving at a consistent speed.
3. Set the Right Chip Load—Stop Guessing, Use Data
Chip load is how much material each tooth on your cutter removes per revolution, right? If you guess this, you’re either under-machining (wasting time) or over-machining (breaking tools). A lot of shops just use the “recommended settings” from the tool manufacturer, but that’s for a generic machine. For my CNC boring and mills, we give custom chip load charts tailored to each machine’s rigidity, spindle power, and tool holding system.
Let’s take a ½-inch carbide end mill for example. A generic chart might say 0.005 inches per tooth, but on our rigid machines with shrink fit tool holders, you can push that to 0.007 inches per tooth, and the tool still holds up longer. How do you calculate your exact chip load? Let’s do the quick math: Chip Load = (Feed Rate) / (Spindle Speed x Number of Teeth). But don’t overcomplicate it—if you’re using our machine’s CAM post, it’s already built in, and we can tweak it on site if you tell us your materials and cutter types. I once had a guy running a CNC boring and mill making mold parts, who was breaking 2 end mills a day because he was running his chip load way too high. We adjusted it to match his machine’s rigidity, and he went 2 weeks without breaking a tool.
Also, for deep boring operations—super common on these machines—you need to adjust chip load as you go deeper. When you’re boring a hole that’s 10 inches deep, the tool can deflect a little, so you need to reduce the chip load by 10-15% to keep the hole straight. If you don’t, you’ll get a tapered hole, which means rework.
4. Optimize Non-Cutting Moves (That’s the Hidden Time Suck)
Here’s a secret: up to 30% of your cycle time is spent on moves where the cutter is not cutting. That’s like driving 10 miles per hour because you stop at every stop sign, even when it’s empty. Non-cutting moves include rapid moves between parts, lifting the cutter between cuts, and moving to clearances.
First, set your safe Z-height correctly. Don’t set it to 2 inches above the part—set it to the minimum height needed to avoid collisions during rapid moves. I’ve seen shops with Z-height set at 4 inches, and that adds up to seconds per part, which is hours a week for a 100-part run. Also, use “rapid traverse smoothing” on your machine—this lets the axes move at a high speed without slamming into each other, so you can lower the Z-height without risking a crash.
Another thing: don’t lift the cutter between every small cut. If you’re machining a series of small holes or a pocket, use “plunge and feed” or “linear linking” instead of lifting the cutter. This keeps the cutter down, so you don’t waste time moving it up and down all the time. The Detroit shop I mentioned earlier cut their non-cutting time by 12% just by fixing their Z-height and turning off unnecessary cutter lifts.
Also, check your axis configuration. Some CNC boring and mills let you prioritize either speed or precision for non-cutting moves. If you’re machining a lot of large, simple parts, prioritize speed—no need for micro-precision on a rapid move. For tight-tolerance aerospace parts, prioritize precision, but you can still tweak it to cut 5% off non-cutting time without losing accuracy.
5. Test and Validate Your Path—Don’t Just Run It Cold
I know you’re in a rush to get parts out, but skipping the simulation step is a recipe for disaster. Most CAM software has a 3D simulation tool, but don’t just watch the cutter move—zoom in on the tool paths, check for gouges, and make sure the tool doesn’t collide with the fixture, the part, or the machine itself. I’ve seen shops run a path that looked fine on simulation, but because they used an old fixture that shifted a little, the cutter crashed and put a 2-inch scratch on a $2000 part.
Also, do a test cut on a scrap piece of the same material before running a full production run. This lets you tweak chip load, speed, and pathing without wasting good material. Last month, a customer of mine was machining Inconel for a gas turbine part, and his initial path had chatter marks. We did a test cut on Inconel scrap, adjusted the spindle speed by 50 RPM, and the chatter was gone. That saved him from reworking 50 production parts.
Another trick: use a trial run at 50% speed first. If the path works at half speed, it’ll work at full speed—plus you can catch any kinks before you push the machine hard.
6. Fix Tool Holding and Rigidity (It Changes Everything)
Wait, this isn’t a path setting, but it directly affects how well your tool path works. If your tool is loose in the holder, or the machine’s workholding is wobbly, no amount of path optimization will make your parts perfect. I always tell customers: a $50 shrink fit tool holder will make your tool path work 20% better than a $10 collet holder. Shrink fit holders eliminate runout, so the cutter cuts evenly, which lets you run faster and get better surface finish.
Also, make sure your workholding is rigid. If your part is shifting during machining, the tool path will be off. For large parts on a CNC boring and mill, use dowel pins instead of just clamps, and make sure the clamps are tightened evenly around the part. A customer making large mold bases told me he had 0.005 inch runout on his bores until he switched to dowel pins, and now his runout is less than 0.001 inch. That’s all workholding, not the machine or path.
Let’s Wrap This Up (No Fluff)
Optimizing tool paths on a CNC boring and milling machine isn’t rocket science, but it’s not something you can set and forget either. It’s about using the right post-processor, matching path strategies to each operation, setting accurate chip loads, cutting down on wasted non-cutting time, testing before production, and making sure your tooling and workholding are solid.
If you’re running into issues with cycle times, tool wear, or part quality, these steps will get you 80% of the way there. At the end of the day, the goal is to make good parts faster and cheaper, right?
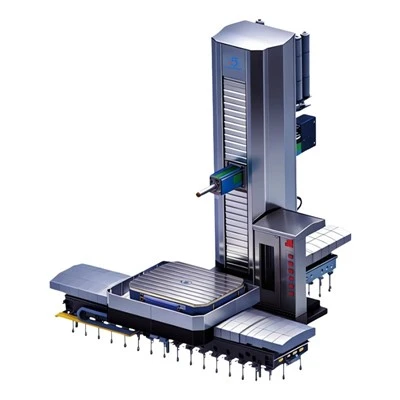
CNC Gantry Boring Mill If you’re currently frustrated with your current CNC setup, or you’re looking for a machine that’s built to make optimizing tool paths easier (trust me, our machines have all the custom post tools and rigidity to make this stuff seamless), I’d be stoked to chat with you. No sales pitch, just straight talk about how we can help your operation run smoother. Just reach out to connect for a no-pressure chat.
References
- Smith, G. (2022). CNC Machining Optimization: Tools, Paths, and Strategies for High-Volume Production. Industrial Press.
- Bosch, T. (2021). Modern CNC Boring and Milling: Rigidity, Tooling, and Path Optimization. Society of Manufacturing Engineers.
- CAMWorks Team. (2023). Best Practices for Post-Processing and Tool Path Validation for Boring Operations. SolidWorks Corporation.
- Aerospace Manufacturing Association. (2022). Tool Path Optimization for Tight-Tolerance Boring in Exotic Alloys. AMA Technical Bulletin.
5Axis (Shandong) CNC Equipment Co., Ltd.
As one of the most professional CNC boring and milling machine manufacturers and suppliers in China, we also accept customized orders. Please feel free to buy cheap CNC boring and milling machine for sale here from our factory. For price consultation, contact us.
Address: No.2000, Beixin West Road, Jinghe Street, Tengzhou City, Zaozhuang City, Shandong Province
E-mail: summer@good5axis.com
WebSite: https://www.china5axis.com/
